Concrete Batch Plant Components
Concrete batch plant components cover the main equipment used for material storage, weighing, conveying, mixing and process control. Depending on the concrete batching plant type and capacity, the exact layout can vary, but most of them include aggregate bins, weighing hoppers, conveyors, storage silos, conveyors, a concrete mixer and a central control system. Each component handles a specific part of production, and the control system coordinates their operation during batching, feeding, mixing and discharge.
The components normally found in concrete batching plants include:- Aggregate bins and feeders
- Aggregate and powder weighing hoppers
- Cement silos and conveyors
- Water and admixture dosing equipment
- Belt conveyors or skip hoists
- Concrete mixer
- Control system and operator panel
- Dust collection equipment
-
Aggregate Feed System for Concrete Batching Plant
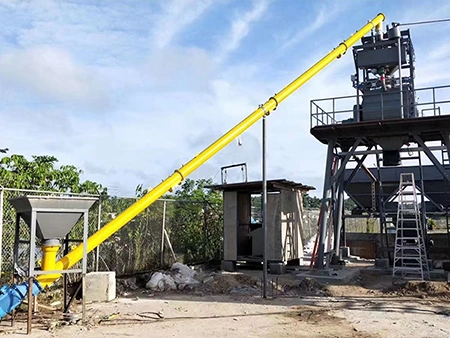
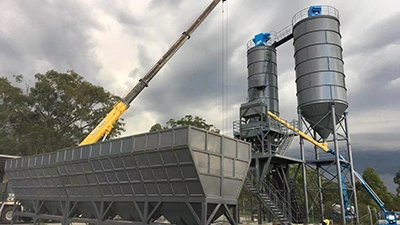
Aggregate feed systems store sand, gravel and other aggregates, measure the required amounts for each batch, and feed them into the concrete production process. Depending on the concrete mix, the aggregate batcher can use 2 to 6 separate bins, so different materials are kept separated until the required amount of each one is measured. The storage bins are positioned above the weighing section, so each aggregate can be measured as it is discharged. After weighing, the discharge belt carries the materials toward the mixer or the next conveyor.
Aggregate Feeding ProcessEach aggregate stays in its own storage bin until the batching process starts. The feed conveyor moves the first material to the weighing hopper and stops when the required weight is reached, then the next aggregate is measured in the same way. After all materials for the batch have been weighed, the discharge conveyor sends them to the next part of the concrete batching plant.
-
Skip Hoist System
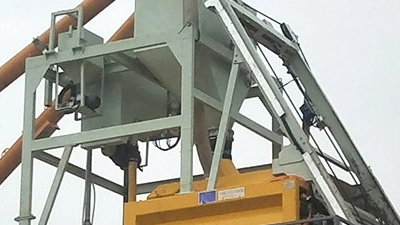
Skip hoist systems move weighed aggregates from the batching section to the concrete mixer using a lifting bucket (also known as skip bucket). The bucket moves along a guided rail, lifts the materials to the mixer and discharges them into the mixer once it reaches the top. Skip hoists are suitable when the batching plant needs a more compact aggregate feeding system. Since the bucket lifts the weighed aggregates directly to the mixer, the concrete plant does not need the long conveyor layout used on belt-fed systems.
-
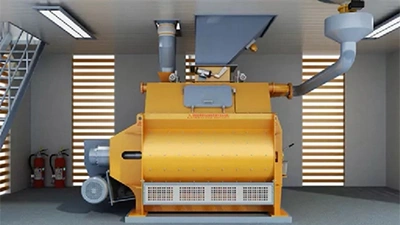
Twin-Shaft Concrete Mixer
Twin-shaft concrete mixers have two horizontal mixing shafts fitted with multiple arms and blades to mix aggregates, cement, water and other ingredients into a uniform concrete batch. The two shafts rotate at the same time, so the materials move through the mixing chamber quickly and are blended from different directions. This type of mixer is suitable for high-volume concrete production and applications that need fast mixing with consistent results.
-
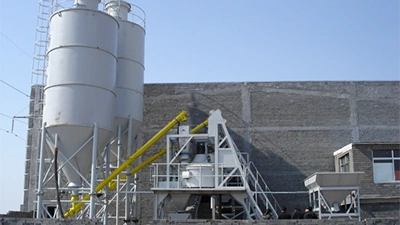
Cement Storage Silos
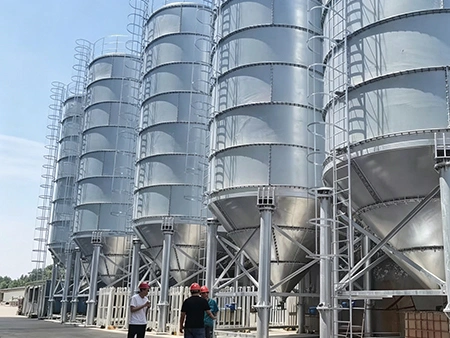
The cement silos provide enclosed storage for cement, fly ash, mineral powder and other bulk powder materials. The capacities vary from 30 to 2,000 tons. Our wide range of bulk storage silos gives customers different options based on required storage capacity, available installation space, transportation requirements and site conditions.
-
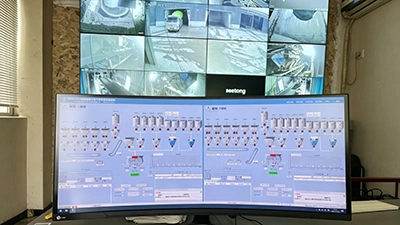
Electrical Control System and Control Room
Operators can switch between automatic and manual modes while viewing batch proportions, production output and fault alarms in real time. Remote monitoring provides access to the same plant information when operators are off site.